 Engineering Library
 Engineering Library
This article is part of our Engineering Library on oil seal failure diagnosis and reliability improvement.
Continue Reading This Series
📖Part 1: Why Oil Seals Really Fail Before Their Expected Service Life
📖Part 2: Lip Wear Patterns and What They Reveal About Oil Seal Failure
📖Part 3: How Different Failure Modes Shape Oil Seal Lip Wear Patterns
📖Part 4:Shaft Surface Damage vs Oil Seal Failure: Which Comes First?
📖Part 5:Oil Seal Failure Analysis: 30 Failure Scenarios, Diagnostic Checks, and Corrective Actions (Current Article)
Quick Answer
Oil seal failure analysis starts by locating the leakage path, recording operating conditions, and inspecting the seal, shaft, housing, and lubricant together. Lip wear, hardening, cuts, swelling, or outer-diameter damage provide clues, but a wear pattern alone rarely confirms the root cause. Corrective action should address the verified problem and be checked under representative operating conditions.
How to Read These Oil Seal Failure Scenarios
A typical scenario describes a plausible failure mechanism and a way to investigate it. A documented field case needs traceable evidence: what was installed, what happened, what was measured, what changed, and what happened afterward.
Keep three levels of confidence separate:
- Suspected: The symptom fits a mechanism, but competing explanations remain.
- Supported by inspection: Measurements or physical evidence support the mechanism, although its contribution may remain uncertain.
- Verified by testing: A defined test supports the diagnosis or corrective action within its stated conditions. This does not establish performance under every operating condition.
For example, a cut lip supports mechanical damage. It does not establish whether the cut occurred during installation, operation, or removal. An installation trial with an inspected shaft and controlled handling can help resolve that question.
Use one record per failure. A compact form is easier to maintain than an investigation reconstructed from disconnected photographs.
| Record section | Information to retain |
|---|---|
| Application and seal | Equipment, location, markings, dimensions, profile, compound, batch if available |
| Operating conditions | Speed, fluid, temperature, pressure, orientation, load cycle, environment |
| Observed evidence | Leakage path and timing; seal, shaft, bore, and lubricant condition |
| Diagnosis and verification | Suspected cause, alternatives, measurements, test method, confidence level |
| Action and follow-up | Changes made, acceptance criterion, operating exposure, result and unresolved limits |
Record missing information as unknown. Avoid turning a visual impression into a measured result. If several changes are made together, a successful repair supports the combined intervention; it may not identify which change mattered most.
What to Record Before Removing a Leaking Oil Seal
Locate the Leakage Path
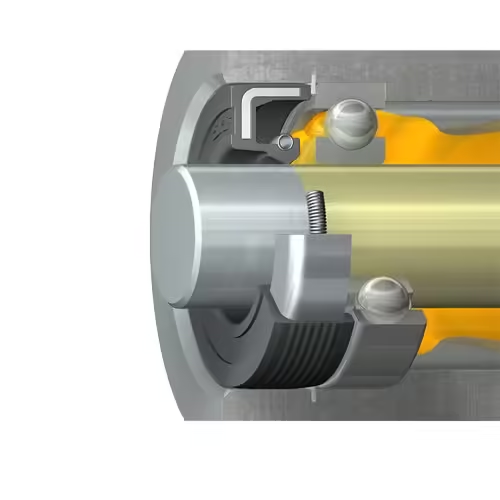
First identify where fresh oil appears. Leakage can cross the shaft-to-lip interface, travel between the seal outer diameter (OD) and housing, or originate from a nearby joint. Oil running down a housing can make a cover gasket, plug, or split line look like a shaft-seal leak.
Document the assembly before cleaning it. Then clean the accessible area and observe fresh wetting during a safe, controlled inspection. Note whether leakage begins at rest, during startup, at operating temperature, under load, or after shutdown. Do not inspect close to exposed rotating components while machinery is running.
An oil trail on the seal face is not conclusive by itself. Rotation, gravity, and airflow can move fluid away from its original exit point. Where necessary, use an equipment-approved tracing method and inspect adjacent joints.
Preserve the Evidence
Photograph the installed face, surrounding contamination, and shaft position. Mark the seal’s orientation and identify its oil-facing side. Record the installation depth before extraction, especially if the replacement may have contacted a different shaft track.
Retain lubricant identification, recent maintenance history, time to first leakage, and previous replacement intervals. Save a representative oil sample before draining when contamination or fluid degradation is suspected.
Remove the seal without levering across the working lip where practical. Photograph it immediately and identify extraction marks. Preserve deposits before cleaning; if chemical analysis is needed, ask the laboratory about handling and packaging first. Keep the failed seal, spring, and any fragments together, separately from unused comparison parts.
SKF’s seal-analysis guidance treats the seal, mating components, operating environment, and installation as interacting factors. That system-level perspective is more useful than judging the removed rubber alone.
30 Oil Seal Failure Scenarios to Investigate
Installation and Assembly Problems — Scenarios 1–6
1. Immediate leakage after crossing an unprotected keyway or spline
A local cut and leakage from first operation suggest installation damage. Debris trapped during assembly or damage during removal can produce similar marks. Compare the cut location with the shaft’s sharp features and inspect the assembly path. If contact is confirmed, correct burrs and use a suitable smooth installation sleeve. Replace the damaged seal and check the assembly method on an unused sample before returning to production.
2. A folded or inverted sealing lip after shaft insertion
A turned-back lip can leave an incomplete sealing contact. Possible triggers include poor lead-in geometry, off-center shaft entry, unsuitable insertion direction, or friction during assembly. Pressure distortion is an alternative explanation. Check the lip immediately after a controlled assembly trial and review the insertion sequence. If assembly causes the fold, revise the guide tooling and lead-in, following the selected seal’s installation instructions.
3. A displaced garter spring found during inspection
A spring outside its groove can reduce or unevenly distribute lip loading. It may have moved during assembly, operation, or extraction. Photograph its position before disturbing it and inspect the spring groove, insertion path, and handling process. If controlled assembly displaces the spring, correct tooling or insertion conditions. If displacement occurs only during operation, investigate pressure and lip deformation rather than treating spring replacement as the complete repair.
4. Uneven seating from a seal installed at an angle
Different face-to-housing distances around the circumference suggest tilted installation. A distorted housing reference face can mislead the inspection, so establish a reliable datum. Check seating depth at several positions and inspect driver contact marks. If the driver applies uneven force, use a guided tool that loads the supported seal case uniformly. Confirm seating against the drawing; driving every seal flush is not a universal requirement.
5. Incorrect orientation for the intended sealing function
An apparently undamaged seal may leak because its functional direction was misunderstood. For many conventional oil-retention seals, the spring-loaded primary lip faces the retained oil, but exclusion duties and special arrangements differ. Compare the installed section with the supplier’s drawing and actual pressure direction. Check rotational requirements for directional designs. If orientation is wrong, revise both the installation instruction and the assembly inspection, then install a new seal correctly.
6. Outer-diameter damage from a burred housing bore
Shaved rubber, axial scratches, or distorted case edges can indicate damage during pressing. Similar evidence may result from extraction. Inspect the bore entrance, chamfer, dimensions, and tool alignment, then compare the installed condition with a controlled trial. If bore defects are responsible, restore the entrance and fit to specification before replacement. Sealant cannot correct an oversized, oval, or mechanically damaged housing.
Shaft and Housing Problems — Scenarios 7–12
7. A replacement seal leaks on an existing shaft groove
The new lip may run directly in a worn track. Measure the groove and identify the actual contact position; apparent groove depth under side lighting is unreliable. Also inspect bearing movement and installation damage. If the track is unsuitable, evaluate shaft replacement, approved resurfacing, or a compatible repair sleeve. Moving the lip axially is acceptable only when the assembly drawing, surface condition, clearances, and lubrication permit it.
8. Lip damage beside shaft corrosion or pitting
Rust or pits can interrupt the oil film and damage the contact edge. However, corrosion may have developed after leakage allowed water ingress. Examine the pit location relative to the wear track and review storage, washdown, and fluid history. If the running surface is defective, restore or replace it and address the moisture route. Changing rubber alone leaves the damaged counterface in service.
9. Rapid wear with unsuitable shaft surface texture
A rough track can abrade the lip, while an unsuitable very smooth surface may impair lubrication. Measure the surface with an appropriate method and compare it with the specific seal’s counterface requirements. Check texture direction and isolated defects as well as arithmetic average roughness, Ra. If texture is unsuitable, specify a controlled finishing process. A shaft that looks polished is not necessarily a suitable sealing surface.
10. Leakage suspected to involve machining lead
A helical surface feature can transport oil along the shaft, sometimes without severe visible lip damage. Leakage linked to rotation direction is a clue, but directional lip features or fluid circulation can also matter. Review the finishing process and use an appropriate lead-assessment method. If harmful lead is established, correct the counterface process and verify leakage under the application’s permitted rotation directions.
11. Uneven contact with shaft-to-bore misalignment
A fixed offset between shaft and housing centers can load one part of the lip more heavily. Tilted installation, bore distortion, and directional contamination can also create uneven wear. Measure the shaft-to-bore relationship from appropriate datums and inspect seating independently. If the offset exceeds the selected design’s capability, correct component alignment or machining. A different seal should not be expected to compensate for an undefined geometric error.
12. Intermittent leakage with shaft runout or bearing movement
Leakage appearing under load or at particular speeds may involve movement the lip cannot follow. Static alignment can still appear acceptable. Measure runout near the sealing track and assess bearing clearance, shaft deflection, and load-dependent motion. Compare the measurement convention with the supplier’s limit. Correct the source of excessive movement first, then verify operation through the relevant speed and load cycle.
SKF’s shaft-seal technical guidance distinguishes fixed shaft-to-bore offset from dynamic runout and discusses surface characteristics beyond a single roughness figure. Use the requirements for the selected product rather than transferring tolerances from an unrelated seal family.
Lubrication and Thermal Problems — Scenarios 13–18
13. Early lip damage after a poorly lubricated startup
Rapid initial wear or heat distress can follow inadequate lubrication at first rotation. Excessive interference, a rough shaft, and chemical effects remain alternatives. Review preparation and the time required for operating oil to reach the contact. If a dry start is supported, use the approved assembly lubricant and startup procedure. Conventional elastomeric lip-seal practice should not automatically be applied to special dry-installed polytetrafluoroethylene (PTFE) designs.
14. Lip distress where oil does not reach the contact zone
The gearbox may contain adequate oil while the seal contact receives little supply. Internal shields, bearing arrangements, return passages, or machine inclination can affect delivery. Examine the local oil path and reproduce the relevant orientation and speed. If starvation is confirmed, correct supply or drainage through an approved assembly change. Adding a stronger spring or another contacting lip can increase friction without restoring lubrication.
15. Leakage associated with an incorrect lubricant level
Overfilling may increase churning, aeration, or local exposure; underfilling can reduce lubrication and increase component temperatures. These effects depend on equipment layout. Verify level using the manufacturer’s specified machine position and checking procedure. Compare fluid quantity with maintenance records and inspect breather function separately. If level is incorrect, restore it and investigate the filling practice rather than assuming the seal itself requires redesign.
16. Hardening and cracking after sustained thermal exposure
A stiff, cracked lip is consistent with aging, but heat, fluid chemistry, and compound formulation may interact. Compare a failed sample with an unused part of known identity and review temperature excursions, not only average readings. If thermal capability is inadequate, reduce the heat source or evaluate a suitable compound. A higher temperature material still needs compatible fluid behavior and sufficient low-temperature flexibility.
17. Deposits around the lip in a hot-running assembly
Deposits can interfere with contact or lip movement. They may originate from lubricant degradation, contamination, additives, or assembly products. Preserve a sample and examine the oil history and deposit composition where justified. Check whether deposits precede leakage or accumulate afterward. If fluid degradation is supported, address its cause and maintenance practice. Cleaning the visible deposits alone may leave the same conditions ready to recur.
18. Overheating after changing lip interference or spring specification
More radial loading can change friction, contact conditions, and heat generation. A different rubber compound or lip geometry may have changed simultaneously. Compare drawings, spring specifications, shaft dimensions, and controlled operating behavior. If excess loading is established, restore or develop a validated specification. Do not shorten a garter spring as an improvised leakage repair; increased contact force is not automatically improved sealing.
The distinction between scenarios 13 and 14 matters: a startup problem concerns the first operating period, while continuing starvation remains after startup. Treating both with assembly grease may hide the second problem temporarily without resolving it.
Contamination and Environmental Problems — Scenarios 19–24
19. Abrasive wear in a dusty agricultural gearbox
Grit near the lip and abrasive tracks suggest contamination, but particles may enter through breathers, service openings, or assembly handling. Inspect external deposits, lubricant, and the exclusion arrangement together. Compare particle characteristics when useful. If the shaft opening is the route, evaluate shielding or an appropriate exclusion system. If particles originate inside the gearbox, changing only the external dust lip will not remove their source.
20. Mud and water ingress at a rotary tiller shaft
Mud accumulation, corrosion, and water-contaminated oil warrant investigation of the shaft opening. Housing joints, breathers, and condensation are alternatives. Record immersion depth, cleaning practices, debris wrapping, and operation in wet soil. If the seal arrangement is inadequate for verified exposure, evaluate a suitable agricultural sealing system with controlled lubrication. Extra contacting lips require review of heat, space, trapped cavities, and contaminant management.
21. Deterioration after repeated high-pressure washdown
A leakage pattern following cleaning may involve water forced past the exclusion system, detergent exposure, or damaged surrounding protection. Record nozzle direction, distance, cleaning temperature, and chemical identity. Inspect other possible entry routes. If direct spray at the shaft opening is responsible, revise cleaning practice and shielding. If the exposure is unavoidable, select and validate a sealing arrangement for that cleaning duty.
22. Lip scoring with metallic debris in the lubricant
Metal particles can damage the contact and shaft, but they may also be a consequence of existing component wear. Inspect bearings, gears, and other internal sources, and retain oil samples. Distinguish manufacturing residue from particles generated during service. If internal wear is confirmed, repair the originating component and clean the system appropriately. Installing a new seal in contaminated oil leaves the abrasive exposure unchanged.
23. A damaged exclusion lip followed by primary-lip contamination
A torn auxiliary lip can allow dirt to reach the oil-retaining contact. Check for rubbing guards, shaft shoulders, wrapped fibers, unsuitable assembly tools, and packed debris. Confirm whether damage happened in service or extraction. If mechanical interference is responsible, correct the clearance or protection geometry. A thicker exclusion lip must still suit the available space, contact speed, and lubrication conditions.
24. Shaft corrosion after outdoor storage or prolonged shutdown
Leakage after restart may follow corrosion at a stationary lip contact or an exposed shaft section. A shutdown also allows condensation or external water accumulation. Compare the corrosion pattern with the parked seal location and inspect storage records. If storage exposure is responsible, repair the running surface and revise preservation and drainage. Increasing lip loading against a corroded track does not restore the surface.
Material, Pressure, and Specification Problems — Scenarios 25–30
25. Swelling or softening after incompatible-fluid exposure
An enlarged, softened lip suggests material-fluid interaction, but visual comparison alone is insufficient. Confirm the compound and actual fluid, including additives and contamination. Where needed, compare dimensional, mass, hardness, and mechanical-property changes with unused material under defined conditioning. If incompatibility is established, select and test another compound. Nitrile butadiene rubber (NBR) and fluoroelastomer (FKM) describe material families, not identical performance across all formulations.
26. Deterioration after a lubricant or cleaning-agent change
A timing relationship identifies a useful lead, not proof. Review product names, additive packages, mixing history, cleaner concentration, and exposure temperature. A process change may also have altered lubrication or operating heat. Compare old and new conditions through a suitable compatibility and functional evaluation. If the change is responsible, approve a compatible seal-fluid combination or a controlled process revision before production release.
27. Cold-start leakage requiring flexibility investigation
A lip may not follow shaft movement adequately at low temperature even when warm operation is satisfactory. Cold oil behavior, pressure transients, shaft movement, and installation damage remain alternatives. Record the actual soak temperature and first operating cycle. If compound flexibility is limiting, evaluate an appropriate low-temperature formulation and test the complete startup sequence. A generic material temperature range does not define sealing performance in that assembly.
28. Leakage with pressure buildup and a restricted breather
Hot-running leakage can coincide with poor venting, but internal pressure needs measurement. Inspect the breather, its location, connected passages, oil level, and contamination. Record pressure across the relevant duty cycle using an appropriate method. If a restriction causes the problem, restore the approved ventilation arrangement. Do not create an improvised open vent where environmental exclusion or equipment requirements demand a controlled breathing system.
29. Lip distortion beyond the selected seal’s pressure capability
A distorted lip or shifted seal can indicate excessive differential pressure, including brief spikes. Incorrect fit, assembly damage, and thermal effects can look similar. Obtain pressure data near the seal cavity and compare it with the specific design’s combined operating limits. If pressure is excessive, correct its source or evaluate a pressure-capable system. A thicker case or harder rubber alone does not establish pressure suitability.
30. Repeat failure after selecting by dimensions alone
Two seals with matching nominal dimensions can differ in compound, lip geometry, loading, directionality, OD construction, and exclusion function. Compare the old and new drawings and purchase specifications, then inspect application changes and possible part defects. If substitution removed a required feature, define that feature in the replacement specification. Where a batch issue is suspected, retain unused samples and request traceable dimensional and material review.
Diagnostic Matrices: Choosing the Next Check
These matrices summarize the distinguishing checks above. Each action applies only after its stated condition is supported.
| Scenario | Evidence and competing explanation | Distinguishing check | Action if confirmed |
|---|---|---|---|
| 1. Keyway cut | Local cut; extraction damage possible | Match mark to assembly path | Protect sharp features |
| 2. Folded lip | Inverted edge; pressure distortion possible | Inspect controlled assembly | Revise lead-in and guidance |
| 3. Loose spring | Displacement; timing unknown | Observe assembly and service separately | Correct displacement source |
| 4. Tilted seating | Unequal depth; datum may be distorted | Measure from reliable reference | Use guided driver |
| 5. Wrong orientation | Early leakage; damaged contact possible | Compare drawing and fluid direction | Correct orientation instruction |
| 6. OD damage | Shaving; extraction marks possible | Inspect bore and pressing trial | Restore bore entrance and fit |
| 7. Worn track | Groove; bearing movement possible | Measure track and contact position | Repair running surface |
| 8. Pitted shaft | Corrosion; sequence uncertain | Map pits and moisture history | Repair surface and ingress route |
| 9. Poor texture | Rapid wear; excess loading possible | Measure texture against specification | Control finishing process |
| 10. Machining lead | Rotation-linked leak; directional lip possible | Assess lead and lip directionality | Correct harmful shaft lead |
| Scenario | Evidence and competing explanation | Distinguishing check | Action if confirmed |
|---|---|---|---|
| 11. Fixed offset | Uneven contact; tilted seal possible | Measure shaft-to-bore geometry | Restore alignment |
| 12. Dynamic movement | Load-linked leak; lubrication possible | Assess runout and bearings | Correct movement source |
| 13. Startup starvation | Early distress; rough shaft possible | Review first-rotation preparation | Approve startup lubrication |
| 14. Local starvation | Dry contact; supply route uncertain | Inspect local oil delivery | Correct supply path |
| 15. Wrong oil level | Heat or aeration; vent restriction possible | Check prescribed filling procedure | Restore specified level |
| 16. Thermal aging | Hardness and cracks; chemistry possible | Compare samples and thermal history | Reduce heat or qualify compound |
| 17. Deposits | Lip buildup; source uncertain | Analyze deposits and fluid | Address degradation source |
| 18. Excess loading | Heat after revision; compound also changed | Compare drawings and friction behavior | Validate contact loading |
| 19. External grit | Abrasion; internal particles possible | Identify contamination route | Improve relevant exclusion |
| 20. Mud and water | Wet oil; joints or breather possible | Trace entry under relevant exposure | Qualify agricultural arrangement |
| Scenario | Evidence and competing explanation | Distinguishing check | Action if confirmed |
|---|---|---|---|
| 21. Washdown | Post-cleaning ingress; chemistry possible | Review spray and cleaning products | Revise cleaning or protection |
| 22. Metallic debris | Scoring; source component uncertain | Inspect oil and internal components | Repair source and clean system |
| 23. Excluder damage | Torn lip; extraction possible | Check clearances and debris | Remove interference |
| 24. Storage corrosion | Restart leak; water source uncertain | Map parked contact and rust | Improve preservation |
| 25. Incompatibility | Softening; compound identity uncertain | Defined comparison testing | Qualify compatible compound |
| 26. Fluid change | Timing link; heat also changed | Compare fluids and conditions | Approve complete combination |
| 27. Cold startup | Temporary leak; pressure possible | Test actual cold cycle | Qualify cold performance |
| 28. Restricted vent | Hot leak; pressure unmeasured | Measure cavity pressure and venting | Restore approved ventilation |
| 29. Pressure overload | Distortion; poor fit possible | Measure transients and differential | Correct pressure or system design |
| 30. Incomplete substitution | Same size; functional features differ | Compare complete specifications | Define controlled replacement |
Field Experience and Two Case Studies Requiring Records
Agricultural Equipment: Revising the Arrangement After Repeated Leakage
Evidence status: customer-reported improvement; detailed root cause and service-life gain remain unverified.
In a rotary tiller application previously discussed with DRO Rubber Seals, the original TC arrangement reportedly leaked. The replacement was described as a DC arrangement with two spring-loaded primary lips and a thicker exclusion lip. The customer reported improved performance after the change.
Those profile labels describe the products in that discussion; they should not replace a sectional drawing. Similar letter codes can represent different constructions across suppliers.
The engineering question is whether the revised arrangement better matched the actual exposure and operating conditions. Agricultural shafts can experience dust, wet soil, wrapped vegetation, and fluctuating loads. However, the available account does not establish which of these factors dominated this particular failure.
A defensible case report therefore separates three statements:
- Reported observation: The original arrangement leaked and the revised arrangement performed better according to customer feedback.
- Engineering hypothesis: Different contact and exclusion features may have improved performance in that application.
- Unresolved finding: The contribution of lip geometry, shaft condition, installation, lubrication, and operating exposure has not been isolated.
The available information does not include comparable operating hours, measured leakage rates, shaft measurements, compound identification, or a record of simultaneous maintenance changes. It cannot support a percentage reduction in leakage or a quantified life extension.
For a follow-up evaluation, record both sectional drawings, each lip’s function and orientation, lubrication between contacts, and any trapped-cavity pressure. Compare performance under similar field exposure. Additional lips can increase friction or alter cavity behavior, so this report supports application-specific evaluation rather than a general recommendation to add lips.
Gearbox Application: Repeated Leakage After Replacement
Evidence status: proposed case-study slot; no documented customer outcome supplied.
A useful gearbox case would show how mating-component inspection changed the diagnosis. It would need the original leakage location, replacement history, shaft-track condition, bearing measurements, and installation records.
For example, finding a shaft groove creates a hypothesis, but the report should establish whether the new lip actually contacted that groove and whether runout was also excessive. The corrective-action record must identify shaft repair, bearing work, seal changes, and installation changes separately.
Until before-and-after records exist, there is no basis to publish a repaired gearbox, measured bearing defect, or successful service interval as a DRO customer case. Scenarios 7, 11, and 12 provide the investigation framework.
Material Selection: Leakage Following a Fluid or Temperature Change
Evidence status: proposed case-study slot; compound and exposure records required.
This case should identify the original compound, actual operating fluid, temperature history, failure sample, and unused comparison material. A description such as “black rubber failed after an oil change” cannot establish chemical incompatibility.
Useful evidence would include defined property comparisons and a functional test of the proposed replacement in the relevant fluid and operating cycle. The report should state whether the change affected only material or also lip geometry, oil grade, or temperature control.
Without those records, keep the explanation conditional. Neither FKM nor another material family should be presented as the proven solution to an unidentified compatibility problem.
Turning Inspection Findings into Corrective Action
When the Existing Seal Specification May Still Be Suitable
Retaining the current specification is reasonable when evidence identifies a correctable assembly or equipment defect and the seal remains suitable for the duty. Examples include a reproducible installation cut, a damaged shaft track, or pressure buildup caused by restricted approved ventilation.
Also review the seal itself. Dimensional deviation, an inconsistent lip edge, a bonding defect, or the wrong supplied compound can justify supplier investigation. System-level analysis should not become an assumption that every seal is manufactured correctly.
Compare failed and unused parts from the relevant batch where available. Photographs can guide inspection, but they cannot reliably establish compound identity or small dimensional deviations.
When a Different Material or Design Requires Evaluation
Consider a specification change when verified service conditions exceed the current design’s capabilities, exposure has changed, or repeated failures continue after assembly and mating components are corrected.
Evaluate material and structure separately. A fluid-compatibility problem may require another compound while retaining the profile. Contamination may require shielding or a different exclusion arrangement. Pressure may require changes to ventilation or the sealing system. A higher temperature compound does not remove a shaft groove or correct excessive bearing movement.
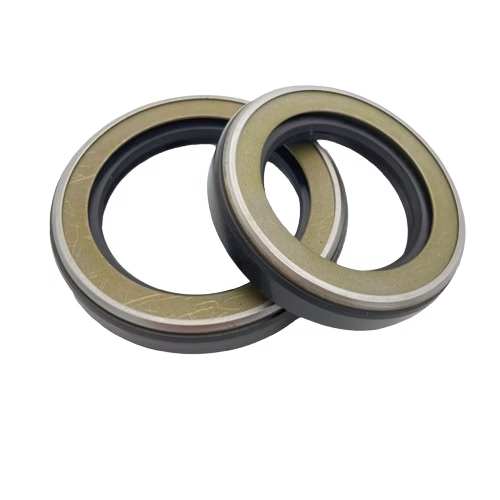
For purchasing, specify the required function and drawing, not simply “better quality.” The DRO oil seal range provides a starting point for profile discussions; the final choice needs application data. Our oil seal materials analysis supports the material comparison stage.
How to Verify the Result
Define acceptance before testing. Depending on the equipment, criteria may concern collected leakage, absence of external drops over a defined exposure, lubricant retention, temperature behavior, or contamination ingress. Distinguish assembly residue from fresh leakage using an agreed inspection method.
Run representative speed, load, orientation, temperature, and start-stop conditions. Include cold startup or washdown if those triggered the original problem. Record exposure in operating hours or cycles; calendar time alone can hide differences in equipment use.
Freudenberg’s rotation-seal testing description includes pressure, temperature, friction torque, speed, leakage, and failure analysis. It supports evaluating the seal-lubricant-system combination under defined conditions rather than judging a replacement only at installation.
| Confirmed finding | Corrective action | Verification method | Acceptance and follow-up |
|---|---|---|---|
| Assembly cut | Correct insertion protection | Inspect controlled assemblies; run functional trial | No assembly damage; agreed leakage limit |
| Unsuitable shaft track | Approved surface repair | Measure repaired track; operate through duty cycle | Drawing compliance and leakage criterion |
| Excess cavity pressure | Restore approved venting or revise system | Measure pressure through representative cycle | Within selected design’s limits |
| Incompatible compound | Qualify seal-fluid combination | Defined material and dynamic tests | Agreed property and functional limits |
| Contamination entry | Correct route and exclusion system | Representative exposure and oil inspection | Agreed ingress and leakage criteria |
Set follow-up intervals from the failure history and maintenance opportunity. Inspect early enough to detect recurrence, then after meaningful duty exposure. A brief leak-free trial is an initial result; it does not demonstrate the intended service life.
What to Send Your Supplier for an Oil Seal Failure Review
Send one consolidated package so the supplier can compare the failed part with its operating environment:
- Seal markings, dimensions, sectional profile, known compound, supplier, and batch information.
- Photographs before removal and close views of the removed lip, OD, spring, shaft track, and housing.
- Equipment type, mounting orientation, rotation direction, and installation depth.
- Shaft speed, load cycle, measured temperatures, and available cavity-pressure records.
- Full lubricant or process-fluid identification, cleaning agents, and recent changes.
- Time to first leakage, when leakage occurs, and earlier replacement history.
- Shaft, bore, runout, alignment, and bearing measurements, including measurement methods.
- Failed sample and an unused comparison sample, where available.
Use How to Measure Oil Seals when dimensions are uncertain. Separate nominal shaft diameter, housing bore, and seal width from measurements taken on worn rubber.
State the required outcome: restore the existing assembly, qualify a substitute, improve contamination control, or investigate a possible batch defect. That makes the review more useful than requesting a price for another same-sized part.
Frequently Asked Questions
Why does a new oil seal leak immediately after installation?
Possible causes include lip cuts, a folded edge, displaced spring, incorrect orientation, tilted seating, OD damage, or a defective shaft track. An adjacent joint can also be mistaken for seal leakage. Locate the fresh leakage path and inspect the assembly sequence before changing material.
Can an oil seal wear pattern identify the root cause?
A wear pattern can narrow the investigation, but usually cannot establish the cause alone. Uneven contact, for example, may involve fixed misalignment, installation tilt, or shaft movement. Match the physical evidence with measurements, service history, and suitable tests.
Why does the same oil seal fail repeatedly?
The original cause may remain in the shaft, housing, bearings, lubrication, pressure, contamination route, or replacement specification. A recurring manufacturing defect is another possibility. Compare repeated failures and unused parts rather than assuming either the equipment or seal is automatically responsible.
How can I distinguish lip leakage from outer-diameter leakage?
Document the assembly, clean accessible surfaces, and observe where fresh oil first appears during a controlled inspection. OD leakage emerges at the housing interface; lip leakage crosses the shaft contact. Rotation and gravity can obscure the path, so a stationary oil trail may be inconclusive.
When should I change the seal material or profile?
Evaluate a change when verified fluid, temperature, pressure, speed, movement, or contamination requirements exceed the current specification. Correct assembly and mating-surface defects as well. Select a compound and profile for the identified problem, then qualify the combination under relevant conditions.
What evidence confirms that a corrective action worked?
Use a predefined leakage or ingress criterion, recorded operating exposure, representative duty conditions, and appropriate follow-up inspection. Document every simultaneous change. A result supports performance only within the tested conditions and duration; longer service-life claims require comparable records.
Conclusion
Effective oil seal failure analysis connects a leakage path with physical evidence, distinguishing checks, and a verified corrective action. Use these 30 scenarios to choose what to inspect next. For a replacement review, send DRO Rubber Seals the failed-part photographs, complete specification, and operating data so the proposed solution addresses the observed problem.
Website: drorubber.com
WhatsApp: +0086 15815831911
WeChat: +0086 13784044874